Maximizing Poultry Farming Efficiency with Large Chicken Cage Systems
Poultry farmers constantly seek ways to improve efficiency, bird health, and overall productivity. One of the most effective solutions is adopting large chicken cage systems, which offer superior space utilization, easier management, and better flock performance compared to traditional floor rearing.
Why Large Chicken Cages Are a Game-Changer
Unlike small battery cages or open-floor systems, large chicken cages are designed to house more birds per unit while maintaining optimal living conditions. A typical setup may hold 60 to 120 birds per cage tier, arranged in multi-level configurations to maximize vertical space.
Farmers using these systems report:
- Higher egg production due to reduced stress and controlled environments.
- Lower feed wastage since feed troughs and nipple drinkers are precisely positioned.
- Easier manure management with droppings collected on belts or trays beneath each tier.
Features of an Effective Large Cage System
1. Durable Construction for Longevity
Galvanized steel frames resist rust and corrosion, even in humid climates. The wire mesh flooring prevents foot injuries while allowing manure to pass through, keeping birds clean. Farmers in tropical regions, where moisture accelerates wear, benefit most from heavy-duty galvanization.
2. Optimized Space per Bird
Overcrowding leads to feather pecking and reduced productivity. Large cages provide at least 450–600 cm² per bird, ensuring enough room for movement without excessive space that encourages aggression. For example, a cage measuring 2m x 1.5m comfortably houses 80–100 layers.
3. Automated Feeding and Watering Systems
Manual feeding in open systems is labor-intensive. Large cages integrate:
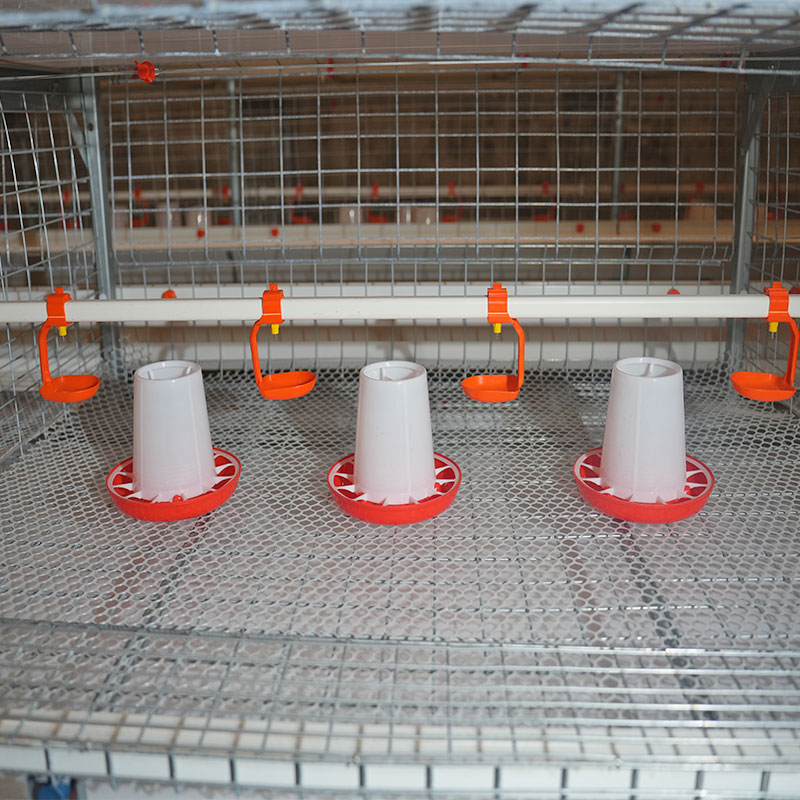
- Trough feeders with adjustable levels to prevent feed spillage.
- Nipple drinkers that minimize water contamination and leakage.
A farm with 10,000 birds can reduce feeding labor by 70% compared to scatter-feeding methods.
4. Efficient Manure Removal
Manure buildup increases ammonia levels, harming respiratory health. Large cages use:
- Scraper belts that remove waste daily.
- Drop trays for farms without automatic systems, requiring manual cleaning every 2–3 days.
Poultry houses with belt systems maintain better air quality, reducing respiratory infections by up to 40%.
5. Multi-Tier Designs for Vertical Farming
Stacking cages in 3–5 tiers maximizes floor space. A 500m² shed can hold 20,000 birds in a 4-tier A-frame system, whereas floor rearing would only accommodate 5,000.
Comparing Large Cages to Alternative Systems
Vs. Free-Range Farming
Free-range systems allow natural behavior but expose birds to predators, diseases, and weather extremes. Large cages provide controlled environments, reducing mortality rates from external threats.
Vs. Conventional Battery Cages
Small battery cages (holding 3–5 birds each) are cheaper but limit movement, increasing bone weakness. Large cages offer better welfare while maintaining high-density farming benefits.
Vs. Deep Litter Systems
Deep litter requires frequent replacement and harbors pathogens. Cages keep birds separated from waste, lowering coccidiosis outbreaks.

Best Practices for Managing Large Cage Systems
1. Proper Stocking Density
Overcrowding stresses birds, reducing egg production. Follow these guidelines:
- Layers: 8–10 birds per m² (cage area).
- Broilers: 12–15 birds per m² for optimal growth.
2. Regular Cleaning and Disinfection
Even with manure belts, residual waste can accumulate. A monthly deep clean with quaternary ammonium compounds prevents bacterial buildup.
3. Lighting Optimization
Light stimulates egg production. Use 16 hours of light daily (natural + LED supplements) at 10–20 lux intensity. Automated timers ensure consistency.
4. Ventilation Control
Poor airflow increases heat stress. Install exhaust fans (1 fan per 200 birds) and side curtains for natural ventilation in warmer climates.
5. Routine Health Checks
Caged birds are easier to inspect. Look for:
- Pale combs (indicating anemia or disease).
- Swollen joints (signs of bacterial infections).
Economic Benefits for Poultry Farmers
1. Higher Return on Investment (ROI)
While large cages have higher upfront costs, they pay off within 2–3 years due to:
- Increased egg/broiler production.
- Lower mortality rates.
- Reduced labor expenses.
2. Lower Feed Costs
Precision feeding reduces waste by 15–20%, saving thousands annually on large farms.
3. Scalability
Farmers can start with a few cages and expand gradually, unlike open systems requiring full barn conversions.
Real-World Success Stories
Case Study: Ugandan Layer Farm
A farm in Kampala switched from deep litter to 3-tier cages, increasing egg production from 65% to 82% in six months. Manure-related diseases dropped by 50%.
Case Study: Brazilian Broiler Operation
A 50,000-bird farm reduced labor costs by 40% after installing automated feeding and manure belts in large cages.
Final Considerations Before Investing
- Evaluate shed height—multi-tier systems need at least 3m clearance.
- Choose cage dimensions based on bird type (layers need more headroom than broilers).
- Test automation systems before full installation to avoid malfunctions.
Large chicken cage systems are transforming poultry farming by boosting productivity, improving bird health, and cutting operational costs. Farmers who adopt these systems gain a competitive edge through efficiency and higher-quality outputs.
1. Drinking system include the water pipes, water pressure adjuster, drinking nipples, Waterline front-end device, dosing system etc, choose them according to customer's needs.
2. High-quality water drinking pipes, pressure regulating valves and water drinking nipples can effectively prevent the water leakage. Drinking system adopt the closed piping system, which can minimize the water pollution.
3. 360-degree drinking nipples provide adequate drinking water for poultry at all stages.
4. The automatic drinking water system mainly adopts the steel ball drinking nipple. lt uses imported high-grad stainless steel, POM resin, and APS engineering material, which is wearing resistant, and the durability can be used for long time.



1. Automatic feeding machine can be chosen between gantry and ladder feeding machine. Gantry type feeding machine is a relatively economical and practical machine with simple operation, remote control walking character, easy to manage.
2. Mechanical transmission device running smoothly, low noise, long service life.
3. With the use of automatic control, the feeding system can adjust the amount of material.
4. Feeding with arched structure, high carrying capacity, not easily deformed.
5. Saving man power, saving feed, greatly improving the efficiency of Large-scale farming.
6. The walking speed of gantry feeding machine is 9--12 m/min.




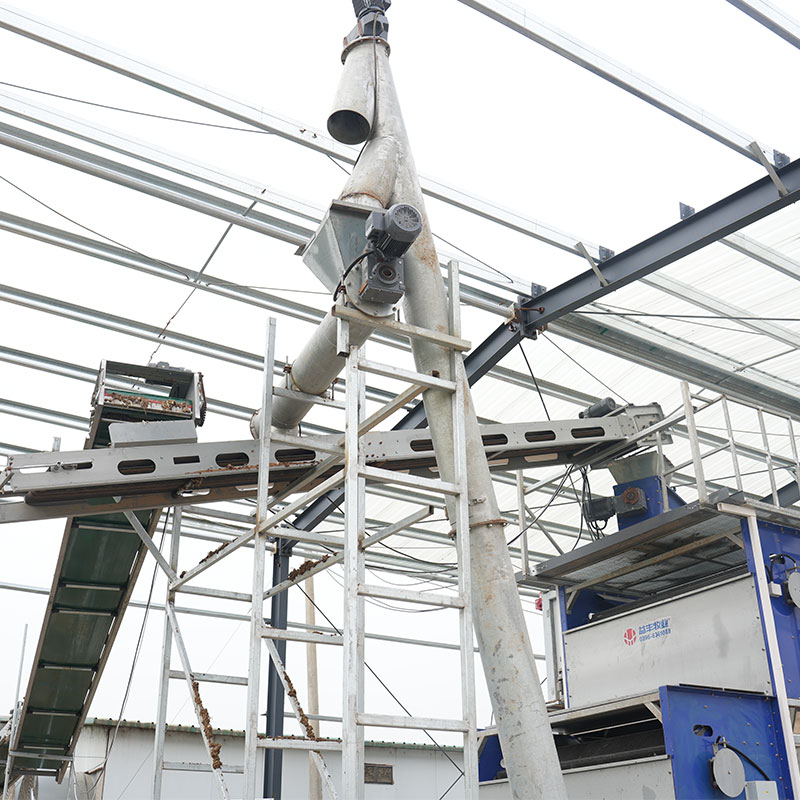
1. Manure removing system included scraper type and conveyor belt type, Which can reduce the labor intensity and labor cost, keep the chicken shed dry and clean.
2. A type chicken cage can use scraper type or conveyor belt type.


3. The scraper type is suitable for A type cages, which can clean two or three rows. For the starters, this type is a good choice. lt can not only save some labor cost, but also save some investment in the whole project. The cleaning speed is 6-10 meters per minute.
4. Conveyor belt type is more suitable for large scale farming. The manure removing belt we use is high quality PP material (polypropylene). The walking speed is 2-4 meters per minute.



High Quality Pellets Made by Mobile Pellet Machine
1. It has professional designed angle of the blade. After the dynamic balance test one by one, the blade can operate smoothly.
2. The air volume is consistent in the whole life of the fan. Bearings has advantage of high strength, low noise, durable and so on.
1. The cooling pads uses high-quality wet curtain paper and adopts space cross-linking technology, which has the advantages of high water absorption, high water resistance, anti-toxicity and long service life.
2. The cooling efficiency is over 80%, without surfactant, natural water absorption, fast diffusion speed and long-lasting effect.
3. The product does not contain phenol and other chemical substances that are easy to cause skin allergies. It is non-toxic and harmless to the human body and chicken when installed and used. It is green, safe, energy-saving, environmentally friendly, economical, and easy to install.
4. The frame aluminum alloy has high strength, good corrosion resistance, durability and beautiful appearance.
5. Use a special filter for the cooling pad at the upper water to ensure clean water quality and support efficient water circulation components.
6. Combined with a negative pressure fan, it can effectively lower the indoor temperature.
The window is made of special selected high-quality engineering plastic, with high strength and long service life, together with superior anti-aging and anti-UV performance.
Function: Ventilation of the chicken house, usually used in the winter.
This system can adjust the wind speed and direction, thus the cold air will not reach chicken directly , which can effectively prevent the phenomenon of cold stress in chicken.
Environmental control system equipment is suitable for large-scale and intensive farming. According to customer requirements, we can provide various types of smart poultry equipment.
1. Our poultry management system is a modular system that manages all aspects of the chicken house, such as climate, temperature, humidity, ammonia, feeding, feed weighing, lighting and ventilation systems, and can monitor the situation of the chicken house in real time through a computer and mobile phone.
2. The management computer is the heart of the poultry farm, allowing you to easily monitor the entire poultry farm.

 WeChat:+8617838608255